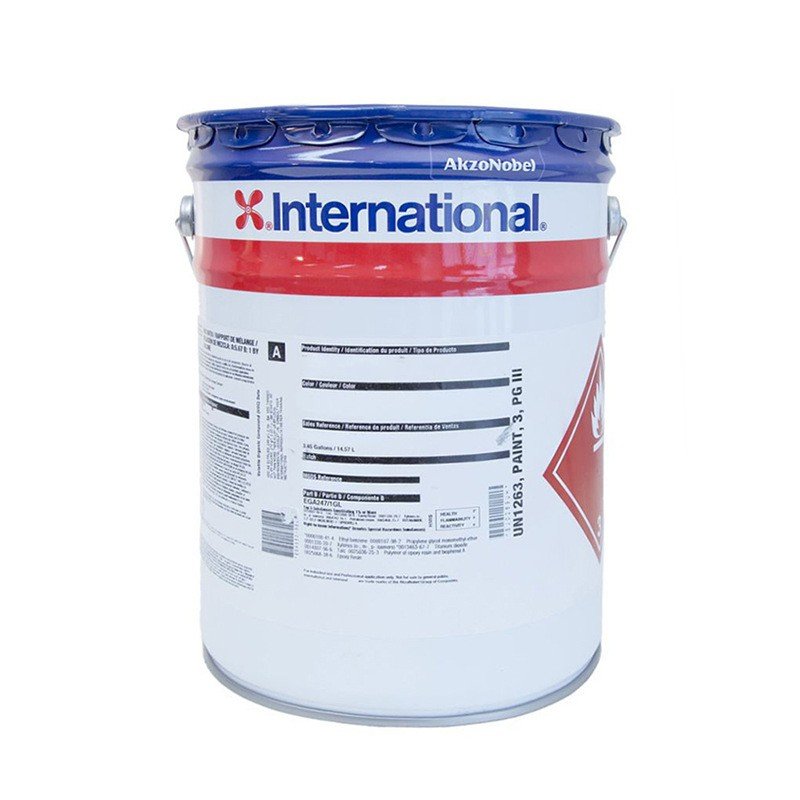
Interline 850 Epoxy Phenolic Storage Tank / Cargo Tank Coating belongs to Epoxy. According to NSF/ANSI/CAN 61 requirements, complies with the applicable health effects standards of NSF/ANSI/CAN 600. A two-component, chemical-resistant, high-solids, thick-film epoxy phenolic storage tank lining coating. For multi-coat application, exposure to low temperatures during or immediately after application may cause incomplete curing and surface contamination, which is detrimental to intercoat adhesion of subsequent coats. Parameters on this page: dry film thickness 100–150 µm (4–6 mils), theoretical spreading rate 6.08 m²/L, number of components two-component.
Parameter source: AKZONOBEL original technical data sheet (TDS) "Interline 850 Epoxy Phenolic Storage Tank / Cargo Tank Coating"; values such as spreading rate are converted from TDS parameters and are for selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 76% |
|---|---|
| Dry Film Thickness | 100–150 µm (4–6 mils) |
| Theoretical Spreading Rate | 6.08 m²/L |
| VOC | 1.88 lb/gal (225 g/L) US EPA Method 24 143… |
| Density / Specific Gravity | 1.57 kg/L (13.1 lb/gal) |
| Number of Components | Two-component |
| Thinner | Normally no thinning is required |
| Mixing Ratio | 4 parts : 1 part (by volume) |
| Colour / Appearance | White, grey, pale yellow, INTERLINE 850 |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
A two-component, chemical-resistant, high-solids, thick-film epoxy phenolic storage tank lining coating.
Provides corrosion protection for the interior surfaces of steel storage tanks containing various products (including: crude oil, unleaded blended gasoline, MTBE, aviation fuel, caustic alkali solutions, potable water and selective aromatic and aliphatic solvents).
When used in potable water tanks, check the current approval certificate information at www.nsf.org.
Meets the applicable health-effects standards of NSF/ANSI/CAN 600, in accordance with the requirements of NSF/ANSI/CAN 61.
Certified to NSF/ANSI/CAN 61
| Colour | White, grey, pale yellow, INTERLINE 850 |
|---|---|
| Gloss | N/A |
| Volume Solids | 76% |
| Typical thickness | Dry film 100–150 µm (4–6 mils), equivalent to wet film 132–197 µm (5.3–7.9 mils) |
| Theoretical Spreading Rate | At 125 µm dry film thickness and the stated volume solids: 6.08 m²/L; at 5 mils dry film thickness and the stated volume solids: 244 ft²/US gal |
| Practical Spreading Rate | Allowing for a suitable loss factor |
| Application Methods | Suitable for airless spray, air spray, brush, roller. Drying time; recommended topcoat recoat interval |
| Temperature | Surface Dry | Hard Dry | Minimum | Maximum |
| 10°C (50°F) | 9 h | 24 h | 30 days¹ | |
| 15°C (59°F) | 8 h | 20 h | 30 days¹ | |
| 25°C (77°F) | 5 h | 8 h | 30 days¹ | |
| 40°C (104°F) | 3 h | 5 h | 21 days¹ | |
¹ The above values apply to closed tank environments. Where there is UV exposure between coats, the maximum overcoating interval shall be shortened. For more details, contact International Paint.
| Flash point (typical) | Component A 42 °C (108 °F); Component B 54 °C (129 °F); mixed 43 °C (109 °F) |
|---|---|
| Product weight | 1.57 kg/L (13.1 lb/gal) |
| Volatile Organic Compounds | 1.88 lb/gal (225 g/L) US EPA Method 24 143 g/kg EC Solvent Emissions Directive content (EU Council Directive 2010/75/EU) 172 g/L Chinese National Standard GB 23985 coating hazard GB 30981.2-S-Pb≤90-C complies with GB 30981.2-2025. For more details, see the "Product Characteristics" section. |
All surfaces to be coated must be clean, dry and free of contaminants. Before painting, all surfaces must be assessed and prepared in accordance with ISO 8504:2000.
Where required, remove weld spatter and grind welds and sharp edges smooth.
Oil and grease must be removed in accordance with the SSPC-SP1 solvent cleaning standard.
Steel structures: this product may only be applied to surfaces abrasive blast-cleaned to Sa2½ (ISO 8501-1:2007) or SSPC SP10. A sharp angular surface profile of 50–75 µm (2–3 mils) is recommended.
Interline 850 must be applied before oxidation of the steel occurs. If oxidation has indeed occurred, the entire oxidized area shall be re-blasted to the standards specified above.
Surface defects exposed during blast cleaning shall be ground, filled or otherwise suitably treated.
If local VOC regulations permit, before oxidation occurs, Interline 850 (thinned 10–15% with GTA220) may be applied to the surface as a primer at a dry film thickness of 40 µm (1.5 mils). Alternatively, dehumidification equipment may be used to maintain the blast standard.
Areas with cracks, damage, welds, etc. shall be treated to the specified standards (e.g. Sa2½ (ISO 8501-1:2007) or SSPC SP10, or power tool cleaning to Pt3 (JSRA SPSS:1984) or SSPC SP11).
Concrete substrates: Interline 850 is also suitable for cementitious surfaces under certain conditions; for details, refer to the product application guide.
| Mixing | For tank application, Interline 850 must be applied in accordance with the International Protective Coatings application guide. This product is supplied as a unit in two containers. Always mix the entire unit in the correct ratio. Once a unit has been mixed, it must be used within the specified pot life. |
|---|
(1) Stir the base (Component A) with a power mixer. (2) Mix all of the curing agent (Component B) with the base (Component A) and stir thoroughly with a power mixer.
| Mixing ratio | 4 parts : 1 part (by volume) |
|---|
| Pot life | 10°C (50°F) | 15°C (59°F) | 25°C (77°F) | 40°C (104°F) |
| 3 h | 2 h | 1 h | 30 min |
| Suitable for airless spray | Recommended nozzle diameter 0.53–0.68 mm (21–27 thou); total paint pressure at the nozzle not less than 176 kg/cm² (2500 psi). |
|---|
| Air Spray | Recommended | Spray gun | DeVilbiss MBC or JGA |
| Air nozzle | 704 or 765 | ||
| (with pressure pot) | Nozzle | E | |
| Brush | Recommended — for small areas only | Typical thickness 50–75 µm (2–3 mil) | |
| Roller application | Recommended — for small areas only | Typical thickness 50–75 µm (2–3 mil) | |
| Thinner | International GTA220 | Normally no thinning is required. |
(or International. In extreme cases, consult the local technical representative.
GTA415 for NSF-approved formulation. Do not thin beyond local environmental regulatory requirements.
unit)
| Cleaner | International GTA853 or International GTA415 |
|---|---|
| Interruption of work | Paint must not be left in hoses, spray guns or spray equipment. Flush all equipment thoroughly with International thinner. Once mixed, paint should not be resealed; if work is interrupted for too long, mix a fresh batch before resuming application. |
| Cleaning | All equipment should be cleaned immediately after use with International thinner. Flushing spray equipment periodically during the daily work is good working practice. Cleaning frequency depends on the volume sprayed, temperature and time spent, including delays. |
All surplus paint and empty containers must be disposed of in accordance with the appropriate local regulations/laws.
Before use, refer to the detailed Interline 850 application procedure.
Interline 850 is generally specified as a 2-coat system with a thickness of 125 µm (5 mils) per coat and a total dry film thickness of 250 µm (10 mils).
The exact scheme for this total dry film thickness depends on the requirements of the final end use. Consult International Paint for specific recommendations on tank lining application.
When used as a primer coat at a dry film thickness of 40 µm (1.5 mils), Interline 850 can maintain a blasted surface for up to 28 days in a semi-protected environment inside the tank. If moisture is present on the surface, oxidation will occur and re-blasting is required. Alternatively, the full coating system may be applied, provided that the recoat intervals are observed and that all surfaces are properly cleaned and prepared before recoating with Interline 850.
For potable water facilities, consult International Paint regarding the permitted degree of thinning.
When the temperature is below 25 °C (77 °F), it is recommended that Interline 850 be allowed to induct for 15 min after mixing before application begins.
Airless spray is the ideal method to achieve the maximum film thickness in a single coat. The required film thickness cannot be achieved by application methods other than airless spray.
With conventional air spray, multiple cross-coats are required to achieve the maximum film thickness. Brush and roller are recommended only for small areas.
The temperature of the surface to be coated must be at least 3 °C (5 °F) above the dew point.
For general use, application of Interline 850 is not recommended when the steel temperature is below 10 °C (50 °F). For potable water storage facilities only, Interline 850 may be applied at steel temperatures of 5 °C (41 °F) and above. Consult International Paint for specific curing procedures.
Ensure adequate ventilation when applying Interline 850 in confined spaces.
For multi-coat application, low temperatures during or immediately after application lead to incomplete curing and surface contamination, harming the intercoat adhesion of subsequent coats.
This product will yellow severely on exposure to sunlight and should not be used on outdoor tanks where colour is an important criterion.
After the final coat has cured hard, determine the dry film thickness of the coating system with a suitable non-destructive magnetic thickness gauge to verify the average total thickness of the applied coating. The coating shall be free from any pinholes or other misses. The cured film must be free from pooling, sagging, runs, inclusions or other defects. All defects and faults shall be corrected. Repaired areas must be re-inspected and cured as specified before the final lining coat is placed in service. For suitable repair procedures, refer to the International Paint Interline 850 application procedure.
For commissioning, refer to the following minimum curing times for Interline 850
| Temperature | Time 1 Time 2 |
|---|---|
| 10°C (50°F) | 7 days 14 days |
| 15°C (59°F) | 4 days 10 days |
| 25°C (77°F) | 2 days 6 days |
| 35°C (95°F) | 36 h 4 days |
| 40°C (104°F) | 24 h 3 daysThe minimum times listed in Time 1 are the minimum curing times at the above substrate temperatures before hydrostatic testing of the tank or immersion in pure aliphatic petroleum products (e.g. diesel or kerosene, but excluding gasoline or gasoline/alcohol blends). The minimum times listed in Time 2 are the minimum curing times at the above substrate temperatures before immersion in the products in the other resistance chemical list. |
The times listed above do not take into account third-party requirements for product curing time, such as for potable water lining use.
For storage of cargoes above ambient temperature, consult International Paint for further detailed advice.
Suitable as a lining for storage of aviation fuel and also suitable for storage of unleaded gasoline.
Interline 850 is not suitable for acidic environments.
This product holds the following specification approvals:• DEF STAN 80-97, for bulk aviation fuel tank lining.
• Spanish Norma INTA 164402-A.
• Norwegian National Public Health Association certificate, for potable water tanks on offshore facilities.
• Certified to AS/NZS 4020:2005, suitable for tanks greater than 42000 mm2/L, with a minimum capacity of 6 L and a minimum internal pipe diameter of 10 cm.
Consult International Paint for specific approved schemes.
Note: VOC values are typical and for guidance only. They may vary with colour and general production tolerances.
Although the low-molecular-weight reactive additive becomes part of the film when cured under normal ambient conditions, analysis by EPA Method 24 shows that it also affects the VOC value.
Generally, where VOC regulations permit, Interline 850 may be used as a self-priming system. In some cases, Interline 982 may also be used. Consult International Paint for specific recommendations.
For other suitable primers/topcoats, consult International Paint.
Consult International Paint to ensure that Interline 850 is suitable for contact with the product to be stored.
| For further information on the industry standards, terms and abbreviations used in this datasheet, see www.international-pc.com | Found in the following documents provided on the website:• Definitions and Abbreviations• Surface Preparation• Coating Application• Theoretical and Practical Spreading Rate• Interline 850 Application InstructionsThe contents of these sections are also available as separate booklets on request |
|---|
This product is intended for professional applicators in industrial use only.
All work, including the application and use of this product, must comply with the relevant national standards, laws and regulations on safety, health and environmental protection.
During application and the subsequent drying period, provide adequate ventilation to keep solvent concentrations within safe limits and prevent fire and explosion (for general drying times, see the product data sheet). Forced ventilation is required in confined spaces. During application and drying, personal ventilation and/or respiratory protection (e.g. air-fed hood or suitable filter mask) must also be provided. Take the necessary measures to prevent skin and eye contact with the coating (e.g. protective clothing, gloves, goggles, mask, barrier cream).
Before use, read and follow the Health and Safety section of the Material Safety Data Sheet and the application procedure for the product (for two-component coatings, those of the base and curing agent).
If welding or flame cutting is performed on metal substrate coated with this product, dust and fumes will be released; use suitable personal protective equipment and local exhaust ventilation.
The specific safety measures depend on the application method and working environment. If these warnings or instructions are not fully understood or cannot be strictly observed, do not use the product and consult the International Paint Protective Coatings division.
| Packaging Specifications | Component A | Component B | ||
| Volume | Packaging | Volume | Packaging | |
| 20 L | 16 L | 20 L | 4 L | 5 L |
| 5 US gal | 4 US gal | 5 US gal | 1 US gal | |
For other packaging sizes, contact AkzoNobel.
| Packaging Specifications | Component A | Component B |
| 20 L | 29 kg | 4.3 kg |
| 5 US gal | 60.2 lb | 8.6 lb |
| Shelf life | At least 12 months at 25 °C (77 °F). |
|---|
Thereafter, inspection is required. Store in a dry, cool environment away from heat and sources of ignition.
© 2026/5/26 AkzoNobel. All rights reserved.
www.international-pc.com
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.
The factory product codes for Interline 850 Epoxy Phenolic Storage Tank / Tank Lining are as follows.Item No.is the most accurate form when ordering;Colour/colour codecorresponds to the actual colour (RAL, GSB are colour chart codes);Packaging SpecificationsFactory complete-set specification format. Colors not listed may be ordered against the colour card.
| Item No. | Colour / colour code | Packaging Specifications |
|---|---|---|
| TLA850 | White | 20 L |
| TLA851 | Grey | 20 L |
This model has a total of2item numbers, all listed on this page; colours outside the table (including special colours and bulk packaging) can be confirmed by phone, delivery dates are advised according to the factory's current production schedule and stock. In the packaging specification, the "+" indicates the complete-set notation for two-component products (base + curing agent), subject to the factory specification; a "—" in the colour column denotes an auxiliary product, or that the item has no colour code in the factory system.