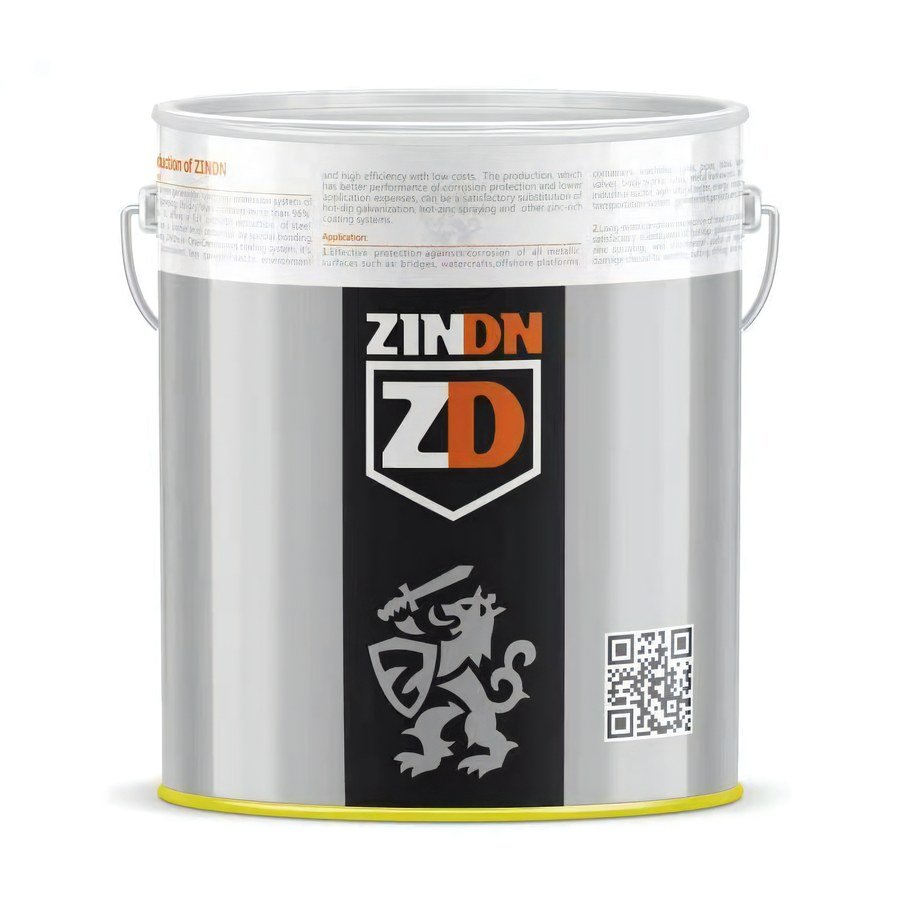
ZD5180 High-solids Polyurethane Topcoat is a polyurethane paint, used as a topcoat. Widely used on metal and non-metal substrates in industrial and marine environments such as petrochemical, bridges, plant buildings and energy, and also on structures requiring decoration. Excellent weather resistance; excellent resistance to atmospheric exposure conditions; good colour and gloss retention. Parameters on this page: volume solids 72 ± 3%, dry film thickness 50/75/150 µm, theoretical spreading rate 4.8 m²/L. Comparable products of the same brand: Aliphatic Polyurethane Topcoat ZD6430, Water-borne Polyurethane Topcoat ZD5200, ZD6310-N01F Epoxy Oil-resistant Antistatic Topcoat.
Data source: ZINDN original Technical Data Sheet (TDS), "ZD5180 High-solids Polyurethane Topcoat"; spreading rate and other values are converted from the TDS parameters, for selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 72 ± 3% |
|---|---|
| Dry Film Thickness | 50/75/150 µm |
| Theoretical Spreading Rate | 4.8 m2/L |
| VOC | ~230 (tested according to GB 30981-2020) |
| Density / Specific Gravity | 1.43 |
| Number of Components | Two-component |
| Flash Point | >25 °C (mixture) |
| Thinner | Thinner ZX-780 |
| Mixing Ratio | Component A (base) : Component B (curing agent) = 9.43:1 |
ZD5180 High-solids Aliphatic Polyurethane Topcoat
ZD5180 High Solids Polyurethane FinishProduct Description:
Two-component, high solids, high-build aliphatic acrylic polyurethane finish
• Excellent weather resistance.
• Excellent resistance to atmospheric exposure conditions. • Good colour and gloss retention. • Cures at temperatures down to -5 °C. • Resistant to splash of mineral oils, vegetable oils, mineral spirits, paraffins, aliphatic petroleum products and mild chemicals.
• Resistant to splash of mineral and vegetable oils, paraffins, aliphatic petroleum productsand mild chemicals•
• Can be over coated even after long term atmospheric exposure• ,
• Good application properties by airless, brush and roller. • High film build-up to 150 µm for one coat. • Can be applied direct to metal.
Widely used on ferrous and non- ferrous substrate for chemistry plants, bridges, industryplants, power etc. industry and marine conditions, as well as decoration needed structures.
| Colour | Standard colours are available, and various colours can be customised to customer requirements. |
|---|---|
| Color | Standard and customer colors |
| Gloss | |
| Gloss | |
| Volume Solids | 72±3% |
| Volume solids | 72±3% |
| Typical mixed density (kg/L)* | 1.43 |
Typical density (kg/L)*: 1.43. *Density can be various due to colour difference.
Typical dry film thickness and theoretical spreading rate
| Minimum | Typical | Maximum | |
| Minimum | Typical | Maximum | |
| Dry film thickness (µm) | 50 | 75 | 150 |
| Wet film thickness (µm) | 69 | 104 | 208 |
| Theoretical spreading rate (m²/L) | 14.4 | 9.6 | 4.8 |
| Theoretical spreading rate (m²/kg) | 10.1 | 6.71 | 3.56 |
| Practical Spreading Rate | Allowing for a suitable loss factor |
|---|
Practical spreading rate: consider appropriated loss factor
| VOC content as supplied (g/L) | ~230 (tested according to GB 30981-2020) |
|---|
VOC(supplied ,g/L): ~230(follow GB30981-2020)
Application Instruction:
| Suitable substrates and surface preparation | Suitable Substrate and Treatment. |
|---|
Substrate Condition:
• Steel; blast cleaned to ISO-Sa2½, blasting profile 40 – 70 µm or power tool cleaned toISO-St3
| • Confirm a compatible preceding coat. | The surface must be clean and dry, with all contaminants removed. |
|---|
• Compatible previous coat must be dry and free from any contamination
| Application and curing conditions | Application and cure condition |
|---|
• During application and curing, ensure the substrate temperature is at least 3 °C above the dew point.
| •Substrate temperature during application and curing should be at least 3°C | above dew |
|---|
point
| • During application and curing, ambient temperature as low as -5 °C is acceptable. | , provided the substrate surface is confirmed to be |
|---|
dry and free of ice.
| •Substrate temperature during application and curing down to -5°C | is acceptable; |
|---|
provided the substrate is free from ice and dry• 85%
• Relative humidity during application and curing should not exceed 85%• ,
• Premature exposure to early condensation and rain may cause color and gloss change
| Mixing ratio by volume | Base : Hardener = 7.3 : 1 |
|---|
Mixing ration (by volume): A(main): B (curing agent) =7.3:1
| Mixing ratio (by weight) | Component A (base) : Component B (curing agent) = 9.43:1 |
|---|
• Mixing two components by stirring homogeneous by stirrer to suitable applicationviscosity by adding suitable thinner.
• Adding too much thinner results in reduced sag resistance and slower cure•
• Must be applied within pot life once mixed.
| Induction Time | No induction required |
|---|---|
| Induction time | No |
Pot life (suitable application viscosity)
| Paint temperature (°C) | 10°C | 20°C | 30°C |
| Pot life (hours) | 4 | 3 | 1.5 |
Application methods
Air Spray
Recommended Thinner: Thinner ZX-780. Thinner usage 10–15% depending on required thickness and application conditions. Nozzle size 1.0–1.5 mm. Nozzle pressure 0.3–0.4 MPa (approx. 3–4 bar; 44–58 p.s.i.). Airless Spray
| Recommended thinner/cleaner | Thinner ZX-780 |
|---|
Recommended Thinner/cleaner: Thinner ZX-780. Thinner usage (by weight) 0–10%, depending on required thickness and application conditions.
Thinner usage(by weight)0 - 10%, depending on required thickness and application conditions 0.43 – 0.48 (0.017 – 0.019 )
Approx. 0.43–0.48 mm (0.017–0.019 in). Nozzle pressure approx. 20.0 MPa (approx. 200 bar; 2901 p.s.i.). Brush/Roller: recommended thinner Thinner ZX-780, thinner % 0–5%.
| Cleaning solvent | ZX-780 |
|---|---|
| cleaner | Thinner ZX-780 |
| Film thickness and theoretical spreading rate | Dry Film Thickness | Theoretical spreading rate by volume (m²/L) | Theoretical spreading rate by weight (m²/kg) |
| Dry film thickness | Theoretical spreading rate by | ||
| volume(m2/L) | weight(m2/kg) | ||
14.4 10.10
50(µm)
| 75 µm | 9.6 6.71 |
|---|
| 75 (µm); 100 µm; 100 (µm) | 75(µm) 7.2 | 75(µm) 5.03 |
| 150 µm; 150 (µm) | 4.8 | 3.56 |
Over coating interval(@75µm DFT)
| Self and compatible finishes | Surface temperature; minimum overcoating interval (hours) | -5°C 24 | 0°C 18 | 10°C 10 | 20°C 8 | 30°C 4 | 40°C 2 |
| Maximum overcoating interval | No limit, but the surface should be clean and free of any contaminants. | ||||||
Note: the above data were measured under good ventilation, typical film thickness and relative humidity ≤75%, for reference only. Actual drying time and the interval before overcoating may be longer or shorter, depending on film thickness, ventilation, humidity, underlying paint, early handling requirements and mechanical strength. Only after the coating is fully cured can it be used in immersed environments, but only for short-term or splash exposure.
above are typical data based on good ventilation, typical film thickness and relativehumidity≤ 75%, just for reference only.
Real drying time base on impact of over coating interval, film thickness, ventilation, humidity,undercoat, ahead of loading and unloading and mechanical requirement etc. Immersiononly allowed after full cure but only for short term or splashing.
Drying/curing table (@75 ㎛DFT)
| Substrate Temperature | Touch dry (h) | Hard dry (hours) | Full cure (days) |
| Substrate | Surface dry(hrs) | Dry to handle(hrs) | Full cure time(days) |
temperature
| -5°C | 20 | 36 | 20 |
| 0°C | 12 | 24 | 14 |
| 10°C | 4 | 18 | 9 |
| 20°C | 2 | 10 | 7 |
| 30°C | 1 | 4 | 3 |
| 40°C | 1 | 3 | 2 |
| Preceding paint | Various epoxy, polyurethane intermediate coats or anti-corrosive primers, |
|---|
| Previous coat | direct to blasted Sa2.5 steel or power tool to St3, various epoxies,polyurethane mid-coats or anti-corrosive primers. |
|---|---|
| Subsequent coat | Various compatible topcoats |
| Next coat | self or various compatible finishes. |
For details, please consult ZINDN company.
Notification;
Must use approved thinner, and overcoat on systemic mid-coats or primers. During paint preparation, contact with water, acid, alkali, alcohol etc. is strictly forbidden. Component B reacts readily with water and alcohols; the packaging drum of the remaining Component B after mixing must be tightly sealed.
During application and drying/curing, the relative humidity must not exceed 80%.
The relative humidity should be no more than 85% when application and curing process.
The appearance will lose gloss, whiten and turn to bad quality once the condensation,sudden temperature drop happened.
Muti coats is needed to achieve enough hiding power with brush and roller application,particular for non-chromatic color pigments like organic yellow, orange etc.
When choosing bright colors such as bright yellow, bright orange etc., the undercoat shouldbe similar or lighter colors to achieve enough hiding power.
Package, Storage and Shelf life
package size
| Components | A (base) | B (curing agent) |
| Container size | 20 L | 3 L |
| Package size (weight) | 21.7 kg | 2.3 kg |
| Package size (volume) | ~14.7 L | ~2 L |
| Flash Point | >25 °C (mixture) |
|---|---|
| Flash Point | >25°C(Mixed) |
| Storage conditions | Store in accordance with national regulations. Keep in a dry, cool, well-ventilated place away from heat and sources of ignition. Keep containers tightly closed. |
Storage condition:must follow national rules. Should be dry, cool, good ventilation andaway heat and fire. The container should be well sealed.
| Shelf life | Shelf life is 1 year under good storage conditions. |
|---|---|
| Shelf life | 1 year at good storage condition. |
Health, Safety and Environment: this product contains flammable substances; site safety shall comply with the relevant national or local government regulations. Note the safety labels on the packaging and read the product Safety Data Sheet (MSDS).
Avoid inhaling solvent vapours and spray mist, avoid contact of paint with skin and eyes, and do not swallow the product. Take the necessary precautions and protective measures for fire prevention, explosion prevention and environmental protection. Use only in well-ventilated conditions. In confined or poorly ventilated areas, provide forced ventilation.
This product contains flammable components; the application site has to meet nationalsafety and local government requirement. More details please read and follow materialsafety data sheet (MSDS)Avoid solvent vapor and paint mist, avoid contacting skin and eyes, forbidden swallowing,
| must | have necessary to have prevention and protection for fire, exploration andenvironment protection solutions. Application under good ventilation, provide sufficientventilation when in narrow space and in non-good air flow. |
|---|
Waste treatment has to follow national and local government requirement.
The product documents and data are based on our experiments and application experience and can be used for application instruction. As the application conditions are usually beyond our control, we only warrant product quality itself. ZINDN keeps the authority to modify for improvement without pre-notification to customers.
| Version information | Revised in July 2025; this data sheet supersedes the previous version. If there are other languages, the Chinese version prevails. |
|---|---|
| Version | Revised in July 2025, this version supersedes the previous version. The other languages are subject to the Chinese technical data sheet. The ZINDN trademark and ZINDN-related marks are the property of the ZINDN Group; no individual or organisation may use them without permission. |
The ZINDN Logo,and ZINDN remarks are properties of group of companies, all thirdparties are not allowed to use without permit.
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.
The factory product codes for ZD5180 High-solids Polyurethane Topcoat are as follows.Item No.is the most accurate form when ordering;Colour/colour codecorresponds to the actual colour (RAL, GSB are colour chart codes);Packaging SpecificationsFactory complete-set specification format. Colors not listed may be ordered against the colour card.
| Item No. | Colour / colour code | Packaging Specifications |
|---|---|---|
| ZD5180 Black | — | 24 KG |
| ZD5180 RAL8022 | — | 24 KG |
| ZD5180 RAL5015 | — | 24 KG |
| ZD5180 RAL3020 | — | 24 KG |
This model has a total of4item numbers, all listed on this page; colours outside the table (including special colours and bulk packaging) can be confirmed by phone, delivery dates are advised according to the factory's current production schedule and stock. In the packaging specification, the "+" indicates the complete-set notation for two-component products (base + curing agent), subject to the factory specification; a "—" in the colour column denotes an auxiliary product, or that the item has no colour code in the factory system.