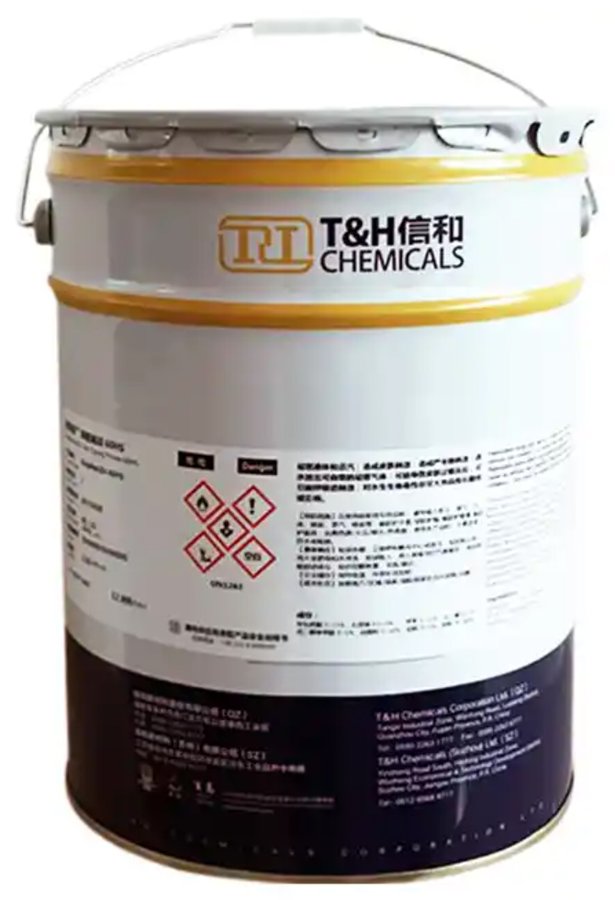
Phenolic Epoxy Static-dissipative Coating XH4216 belongs to Epoxy. Used for anticorrosive protection of steel storage tanks, pipelines and other equipment for high-sulfur crude oil, petroleum intermediate products, MTBE, aliphatic hydrocarbons, some aromatic hydrocarbon solvents and other media. Parameters on this page: Volume Solids 70 ± 2%, Dry Film Thickness 50/80/100 µm, Theoretical Spreading Rate 7 m²/L.
Parameter source: T&H original technical data sheet (TDS) for Phenolic Epoxy Antistatic Coating XH4216; spreading rate and other values are converted from TDS parameters and provided for product selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 70 ± 2% |
|---|---|
| Dry Film Thickness | 50/80/100 µm |
| Theoretical Spreading Rate | 7 m2/L |
| VOC | ≤300g/L |
| Density / Specific Gravity | 1.4 kg/L |
| Number of Components | Two-component |
| Flash Point | 25°C |
| Thinner | 0-15% |
| Mixing Ratio | Component A : Component B = 5.6:1 (by weight), 79:21 (by volume) |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
Two-component high-build phenolic epoxy coating with static dissipative function. Performance complies with the requirements of HG/T 4569 Standard for Static Conductive Coatings for Petroleum and Petroleum Product Storage and Transportation Equipment. Used for anti-corrosion protection of steel storage tanks and pipelines for high-sulfur crude oil, petroleum intermediate products, MTBE, aliphatic hydrocarbons, partial aromatic hydrocarbon solvents and other media. Long-term heat resistance temperature 200 °C under dry conditions.
| Colour | Light grey |
|---|---|
| Gloss | N/A |
| density | 1.4 kg/L |
| Volume Solids | 70±2% |
| Volatile Organic Compounds | ≤300g/L |
| Flash Point | 25°C |
| Mixing ratio | Component A : Component B = 5.6:1 (by weight), 79:21 (by volume) |
| Typical dry film thickness | 100µm×3 |
|---|---|
| Recommended dry film thickness | 200 µm (100 µm × 2) – 400 µm (100 µm × 4), depending on system requirements |
| Induction time (20 °C) | 10~15min |
| Thinner quantity (by volume) | Airless spray 0–10% | Air spray 5–15% | Roller or brush 0–15% |
| Recommended nozzle size | 0.43~0.53m | 2.0~3.0mm | / |
| Recommended spray pressure | 15~20MPa | 0.3~0.6MPa | / |
| Application suitability | Recommended | Applicable | Suitable for small-area repair |
| Dry film thickness (µm) | 50 | 80 | 100 |
| Wet film thickness (µm) | 71 | 114 | 143 |
| Theoretical spreading rate (m²/L) | 14.1 | 8.8 | 7 |
| Temperature | Surface Dry | Hard Dry | Pot Life | Recoat interval | |
| Minimum | Maximum* | ||||
| 10°C | 10h | 24h | 3h | 24h | / |
| 20°C | 3h | 10h | 2h | 12h | / |
| 35°C | 1.5h | 5h | 1h | 12h | / |
*The maximum recoat interval depends on the exposure environment and the end use of the coating.
All surfaces to be coated shall be clean, dry and free of contaminants. Before coating, all surfaces shall be evaluated and prepared in accordance with ISO 8504:2000. Abrasive blast to Sa2½, surface roughness 40–75 µm. Before derusting, remove all oil, grease and welding spatter from the surface and grind welds and sharp edges. Where the coating film surface has suffered mechanical damage and local rusting has occurred, local abrasive blasting to Sa2½ or power tool cleaning to St3 is required before local repair. If this coating is to be applied over an approved old inorganic zinc silicate primer film, the zinc dust coating must be thoroughly removed of chalking or zinc salts before application of this product.
1. During application, ensure ventilation and air exhaust, keep away from ignition sources, and wear protective equipment such as masks and gloves; adequate ventilation shall also be maintained during curing. 2. Before mixing Components A and B, stir Component A uniformly with a power tool, then add the curing agent and mix uniformly; adjust the amount of thinner according to application requirements and temperature changes, stir thoroughly, and induce for 10–15 min before application. 3. Do not use paint exceeding its pot life, otherwise the chemical resistance of the coating will be seriously affected. 4. This product is a surface-tolerant product, suitable only for application over abrasive-blasted steel surfaces and approved zinc dust coating surfaces; it must not be applied over other types of coatings, nor may other coating products be applied over this product's coating, otherwise the static dissipative performance will be affected. 5. During application and curing, the substrate temperature must be above 10°C and at least 3°C above the dew point, and the relative humidity must not exceed 85%. Temperature and relative humidity shall be measured at the substrate near the work site. During application, the paint temperature shall not be lower than 10°C. 6. The recommended thickness per coat of this product shall not exceed 120 µm, otherwise solvent retention in the coating will affect chemical resistance; multiple coats help reduce coating defects and improve corrosion protection performance. At ambient temperature, the film requires 7–10 days of curing before service; at lower temperatures the curing time must be extended (14–21 days) or heating shall be adopted to increase the degree of cure; do not use this product when the temperature is below 10°C. 7. If this coating is to be applied over an inorganic zinc silicate primer surface, the coating must be subjected to a MEK test to ensure the primer is fully cured. 8. Cutting structures coated with this coating will generate smoke and dust; appropriate protection shall be provided. 9. When work is suspended, do not leave paint in paint lines, spray guns or spray equipment. Thoroughly flush all equipment with thinner. If the suspension is too long, it is recommended to remix a fresh batch of paint for application. 10. All equipment shall be cleaned with thinner immediately after use. Periodic flushing of spray equipment during daily work is good practice. Cleaning frequency depends on spray volume, temperature, spray time, including interruption time and other factors. 11. Residual paint and empty containers shall be disposed of in accordance with relevant regional regulations.
| 21.8Kg per set | Component A (base) 18.5 g | Component B (curing agent) 3.3 kg |
| 15.5 L per unit | Component A (base) 12.2 L | Component B (curing agent) 3.3 L |
Keep sealed in a ventilated, cool, dry place away from sources of ignition. Minimum 12 months.
1. For the coating and its recommended thinners, see the safety sheets and the safety data of the relevant materials. This is a solvent-borne coating; avoid inhaling spray mist and solvent vapours, and avoid exposing skin and eyes and contact with uncured paint as far as possible. 2. All work related to the application and use of this product must comply with the relevant national health, safety and environmental standards and regulations.
3. If welding or flame cutting is required on metal coated with this product, dust and fumes will be generated; use appropriate personal protective equipment and adequate local ventilation. 4. If in doubt about the suitability of this product, consult the company.
The information provided in this product data sheet is based on laboratory test results that we consider accurate, and is provided for application guidance only. All recommendations and advice given by T&H on the use of T&H products, whether in technical documents, special consultation or otherwise, are based on information we consider most reliable. Our products and the information provided are intended for users with the necessary knowledge and industrial experience, and it is for these end users to determine whether the products are suitable for their use. T&H cannot control the quality and condition of the substrate, nor the various factors affecting the use of the product. Therefore, T&H accepts no liability for any loss, injury or damage arising from the use of our products or from reliance on this product data sheet (unless otherwise agreed in writing). Data in this product data sheet may be revised as necessary based on practical experience and continued product development.
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.