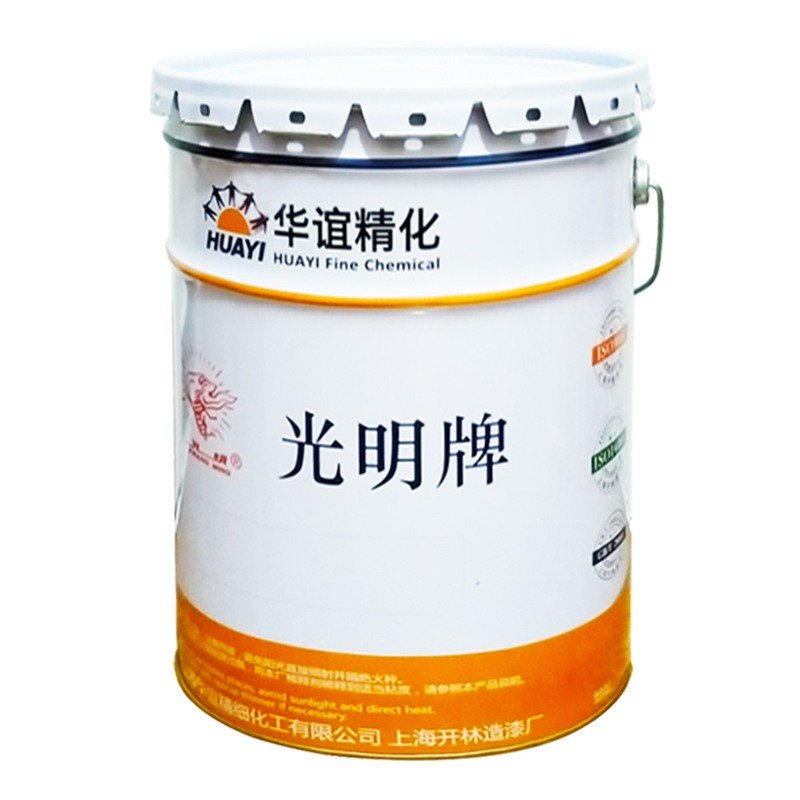
Epoxy Bitumen Ultra High-build Anticorrosive 546 is an epoxy coating used as a primer. Suitable as a heavy-duty anti-corrosion coating for ship bottoms, ballast tanks, wharf steel piles, offshore oil drilling platforms, hydraulic steel gates, mine steel supports, and internal and external pipe walls. A two-component high-performance anticorrosive composed of epoxy resin, coal-tar pitch, epoxy curing agent, anti-corrosive pigment, extender pigment, additives and solvent. One airless-spray coat can achieve a dry film thickness of about 250 µm. Parameters on this page: volume solids 69 ± 3% (after mixing), dry film thickness 250 µm, theoretical spreading rate 470 g/m².
Source: KAILIN original technical data sheet (TDS) "Epoxy Bitumen Ultra High-build Anticorrosive 546"; spreading rate and other values are converted from TDS parameters and are for selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 69 ± 3% (after mixing) |
|---|---|
| Dry Film Thickness | 250µm |
| Theoretical Spreading Rate | 470 g/m² |
| VOC | — |
| Density / Specific Gravity | — |
| Number of Components | Two-component |
| Thinner | Thinner 103 |
| Mixing Ratio | Component A : Component B = 1:1 (by weight) |
| Colour / Appearance | Black |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
Composed of epoxy resin, coal tar pitch, epoxy curing agent, anticorrosive pigments, extenders, additives and solvents
…agent composed of a two-component high-performance anticorrosive.
One airless-spray coat can achieve a dry film thickness of about 250 µm
Suitable for hull bottoms, ballast water tanks, dock steel piles, offshore oil drilling platforms, hydraulic steel gates,
mine steel supports and the inner and outer walls of pipelines, as a heavy-duty anticorrosive coating.
| Appearance | Black |
|---|
| Volume Solids | 69 ± 3% (determined per GB/T 9272 eqv ISO 3233:1998) (after mixing) |
|---|---|
| Mixing ratio | Component A : Component B = 1:1 (by weight) |
| Dry Film Thickness | 250µm |
| Wet Film Thickness | 362µm |
| Theoretical quantity | 470g/m² |
| Flash Point | Component A 22 °C, Component B 22 °C; induction time (after mixing) (20 °C) 30 min |
| Pot life (after mixing) (20 °C) | 8h |
(When the air temperature is above 30 °C, the pot life after mixing the two components shortens as the temperature rises)
| Drying Time | |||
| Temperature | 5°C | 20°C | 30°C |
| Surface Dry | 8h | 4h | 2h |
| Hard dry | 48h | 24h | 16h |
| * Fully cured | 15d | 7d | 5d |
* Below 5 °C, curing stops; not suitable for application
| Recoat interval | |||
| Temperature | 5°C | 20°C | 30°C |
| Minimum | 48h | 24h | 20h |
| Maximum | 15d | 7d | 3d |
| Recommended number of coats | Airless spray 1–2 coats, dry film thickness 250 µm. |
|---|
702 Epoxy Zinc-Rich Shop Primer, 703 Epoxy Iron Oxide Shop Primer, 704 Inorganic Zinc Silicate Shop Primer
Primer, 842 Epoxy MIO Anticorrosive, or applied directly to steel derusted to Sa2.5
Steel surfaces.
When used as a ship-bottom anticorrosive, apply 616 Chlorinated Rubber Iron-red High-build Anticorrosive over 546 as one
coat as a transition layer, then apply 839 Long-life High-build Antifouling to improve the intercoat
adhesion. In applications free from marine fouling, 546 may be used alone.
Mill-scale-free steel: blast clean to Sa2.5, or abrade with a flexible disc to St3
Shop-primed steel: sweep blast or grind corroded areas to St3 with elastic abrasive discs
Areas burned by welding, flame cutting or fairing: remove weld slag and spatter, grind smooth, then abrade with a flexible disc to St3
When the substrate temperature is below 5 °C, the reaction between epoxy and curing agent stops; outdoor application is not recommended, and the winter-grade epoxy bitumen anticorrosive may be selected
| Airless Spray | |
| Thinner | Thinner 103 |
| Thinning quantity | 0–5% (by paint weight) |
| Nozzle tip size | 0.4-0.5mm |
| Spray output pressure | 20–30 MPa (approx. 200–300 kg/cm²) |
| Air Spray | |
| Not recommended for large areas; suitable only for small-area touch-up or small workpieces | |
| Thinner | Thinner 103 |
| Thinning quantity | 0–10% (by paint weight) |
| Nozzle tip size | 2.0-3.0mm |
| Air pressure | 0.2–0.4 MPa (approx. 2–4 kg/cm²) |
Mainly for small-area application and touch-up
| Thinner | Thinner 103 |
|---|---|
| Thinning quantity | 0–3% (by paint weight) |
| Cleaning solvent | Thinner 103 |
| Safety measures | See the Safety Data Sheet (MSDS) of Shanghai Kailin Paint Factory. |
| Packaging | Component A 20 L drum 10 kg, Component B 20 L drum 10 kg |
| Shelf Life | 12 months |
| Film thickness and consumption | ||||
| Dry film thickness (µm) | 50 | 125 | 200 | 250 |
| Theoretical consumption kg/m² | 0.094 | 0.235 | 0.376 | 0.470 |
50µm.
| Notes | To use this product correctly, read the Application Guide in this data sheet carefully. |
|---|
The above information and data for this product are accumulated from our tests and practical experience
accumulated, and may serve as an application guide. For application carried out under conditions unknown to us, we
We guarantee only the quality of the paint itself and accept no responsibility for other matters. We
and reserve the right to make modifications as the product is improved.
Information is subject to the manufacturer's latest version; the manufacturer's latest TDS prevails.
The technical parameters on this page are taken from the product's original manufacturer technical datasheet, the copyright of which belongs to the manufacturer. If a rights holder considers the presentation inappropriate, contact us for verification and handling.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.