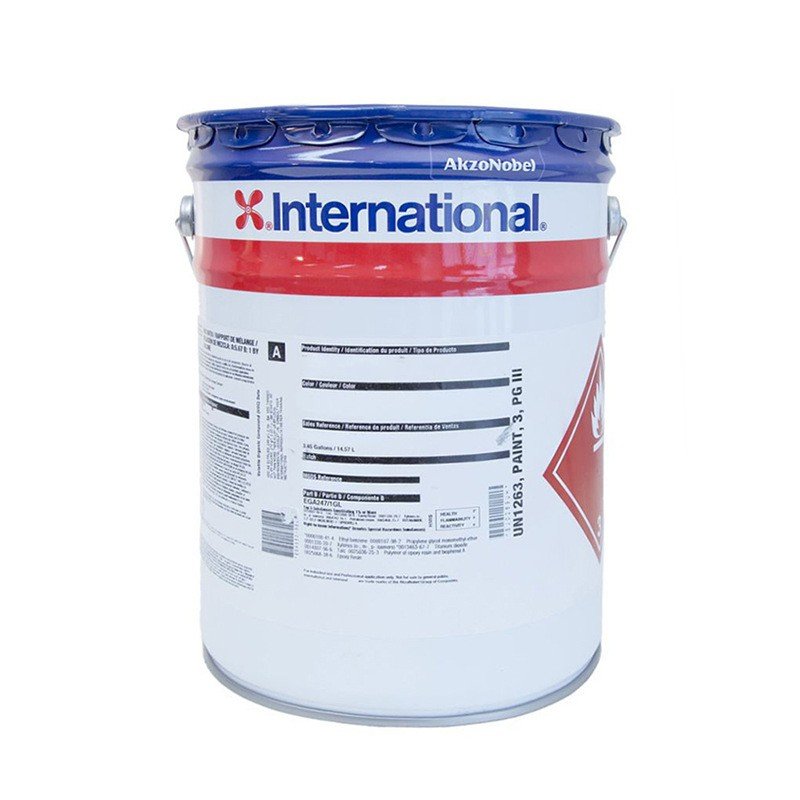
Interdur 8802 Epoxy Zinc Phosphate Micaceous Iron Oxide Primer is an epoxy coating used as a primer. Under most climatic conditions, it can be overcoated within 3 hours, thereby accelerating production and increasing fabrication shop throughput. A two-component epoxy zinc phosphate/micaceous iron oxide primer formulated with unique polymer technology, capable of fast curing and recoating even at low temperatures. A film of 75 µm (3 mil) dry film thickness can normally be overcoated after 6 months of exposure, provided it is suitably cleaned and any damaged areas are repaired. Parameters on this page: dry film thickness 75-100 µm (3-4 mil), theoretical spreading rate 8.93 m²/L, number of components: two-component.
Parameter source: AKZONOBEL original technical data sheet (TDS) for Interdur 8802 Epoxy Zinc Phosphate Micaceous Iron Oxide Primer; spreading rate and other values are converted from TDS parameters and provided for product selection reference only.
The above content is compiled from the manufacturer's datasheet and this site's parameter tables. For selection, coating systems and lead times, pleaseContact Usfor confirmation.
This page carries the full TDS for this product, translated from the manufacturer's original document. No file download is needed; for an original-language copy, send an enquiry.
| Volume Solids | 67% |
|---|---|
| Dry Film Thickness | 75–100 µm (3–4 mils) |
| Theoretical Spreading Rate | 8.93 m²/L |
| VOC | 2.64 lb/gal (317 g/L) US EPA Method 24, 21… |
| Density / Specific Gravity | 1.54 kg/L (12.9 lb/gal) |
| Number of Components | Two-component |
| Thinner | International GTA220 (or Internationa… |
| Mixing Ratio | 3 parts : 1 part (by volume) |
| Gloss | Matt |
For more Q&A on selection, application, acceptance and defect diagnosis, seeFAQsection.
A two-component epoxy zinc phosphate/micaceous iron oxide primer formulated with unique polymer technology that cures and overcoats rapidly even at low temperatures.
A high-solids product with a low volatile organic compound (VOC) content.
Suitable for overcoating within 3 hours in most climates, thereby accelerating production and increasing throughput at fabrication shops.
Also suitable for use on site as a fast-curing maintenance coating.
INTERDUR 8802 micaceous iron oxide grey
| Gloss | Matt |
|---|---|
| Volume Solids | 67% |
| Typical thickness | DFT 75–100 µm (3–4 mil) corresponds to WFT 112–149 µm (4.5–6 mil) |
| Theoretical Spreading Rate | At 75 µm dry film thickness and the stated volume solids: 8.93 m²/L; at 3 mils dry film thickness and the stated volume solids: 358 ft²/US gal |
| Practical Spreading Rate | Allowing for a suitable loss factor |
| Application Methods | Suitable for airless spray, air spray, brush, roller. Drying time; recommended topcoat recoat interval |
| Temperature | Surface Dry | Hard Dry | Minimum | Maximum |
| 5°C (41°F) | 40 min | 4.5 h | 3 h | Unlimited¹ |
| 15°C (59°F) | 30 min | 3 h | 2 h | Unlimited¹ |
| 25°C (77°F) | 20 min | 2 h | 1 h | Unlimited¹ |
| 40°C (104°F) | 15 min | 30 min | Unlimited¹ | |
¹ See Definitions and Abbreviations from the International Paint Protective Coatings division. When polysiloxane topcoats are used, the maximum recoat interval is reduced. For details, consult International Paint.
| Flash point (typical) | Component A 27 °C (81 °F); Component B 28 °C (82 °F); mixed 27 °C (81 °F) |
|---|---|
| Product weight | 1.54 kg/L (12.9 lb/gal) |
| Volatile Organic Compounds | 2.64 lb/gal (317 g/L) US EPA Method 24; 216 g/kg EU Solvent Emissions Directive content, Commission Directive 1999/13; 292 g/L China national standard GB 23985. For further details, see the section on Product Characteristics. |
All surfaces to be coated must be clean, dry and free of contamination. Before painting, all surfaces must be assessed and prepared in accordance with GB 18839-2002.
Remove any oil and grease by solvent cleaning in accordance with GB 18839-2002.
Blast cleaning: blast clean to Sa 2.5 (GB 8923-1:1998). If the steel surface oxidises after blasting and before overcoating with Interdur 8802, the surface should be re-blasted to the specified visual standard. Surface defects exposed by blasting should be ground, filled or treated by a suitable method.
Interdur 8802 is suitable for surfaces initially prepared by blast cleaning as described above, then allowed to degrade naturally under good shop conditions for no more than 7 to 10 days. The surface may degrade to Sa 2, but must be free from loose powdery rust.
Surface defects exposed during blasting must be ground, filled or treated by a suitable method.
Recommended angular surface profile of 50–75 µm (2–3 mils).
Interdur 8802 is suitable for application to blast-cleaned surfaces that originally met the above standard but have been allowed to weather under good shop conditions for 7-10 days. The surface then degrades to Sa 2, but must be free from loose powdery deposits.
Welds and damaged areas of shop-primed steel must be blast cleaned with steel grit to Sa 2.5 (GB 8923-1:1998). If the shop primer has sustained extensive or scattered breakdown, a full sweep blast may be required. If the shop primer has been applied over a blast-cleaned surface, a full sweep blast with steel grit is required before applying Interdur 8802.
| Mixing | This product is supplied in two containers forming one unit. Mix the two components in the specified ratio in one operation. Once mixed, use within the specified pot life. |
|---|
(1) Stir the base (Component A) with a power mixer.
(2) Mix all of the curing agent (Component B) with the base (Component A) and stir thoroughly with a power mixer.
| Mixing ratio | 3 parts : 1 part (by volume) |
|---|
| Pot life | 5°C (41°F) | 15°C (59°F) | 25°C (77°F) | 40°C (104°F) |
| 4 h | 3 h | 2 h | 45 min |
| Suitable for airless spray | Recommended: nozzle diameter 0.43–0.53 mm (17–21 thousandths of an inch); total paint pressure at the nozzle not less than 176 kg/cm² (2503 psi) |
|---|
| Air Spray | Recommended | Spray gun | DeVilbiss MBC or JGA |
| Air nozzle | 704 or 765 | ||
| (with pressure pot) | Spray painting | E | |
| Brush | Applicable — for small-area repair only | Typical thickness 50–75 µm (2.0–3.0 mils) | |
| Roller application | Applicable — for small-area repair only | Typical thickness 50–75 µm (2.0–3.0 mils) |
| Thinner | International GTA220 (or International GTA415) |
|---|---|
| Cleaner | International GTA220 (or GTA 415) |
| Interruption of work | Do not leave paint in hoses, spray guns or spray equipment. Flush all equipment thoroughly with International GTA220. |
Once mixed, paint should not be resealed. If work is interrupted for too long, mix a fresh batch for application.
| Cleaning | All equipment shall be cleaned with International GTA 220 immediately after use. Periodically flushing spray equipment during the daily work is good practice. The frequency of cleaning depends on the quantity sprayed, temperature, spraying time and interruptions. |
|---|
All surplus paint and empty containers must be disposed of in accordance with the relevant local laws/regulations.
Interdur 8802 is preferred in systems for certain chemical environments, because in such environments zinc-containing coatings may be attacked by acids and alkalis.
The maximum recoat interval depends on the integrity of the exposed film. A film at 75 µm (3 mils) dry film thickness can generally be recoated after 6 months of exposure, after suitable cleaning and repair of any damaged areas.
Avoid excessive film thickness, since the adhesion of a topcoat over an aged thick film is not as good as over a film at the specified thickness. When used as a holding primer, avoid excessive film thickness, since intercoat adhesion problems can arise if the subsequent coat is also applied too thickly.
The temperature of the surface to be coated must be at least 3 °C (5 °F) above the dew point.
This product must be thinned only with the recommended International thinner. Other thinners, especially those containing ketones, severely inhibit the curing of the coating.
Interdur 8802 is not suitable for steel structures that may be immersed in water.
In addition to blast-cleaned surfaces, Interdur 8802 can be used on other substrates, such as stainless steel and alloys. Consult International for details.
The intercoat adhesion of a coat applied over aged Interdur 8802 is lower than that over a fresh coat, but it is still adequate for the specified purpose.
Note: VOC values are typical and for guidance only. They may vary with colour and general production tolerances.
The following topcoats/intermediate coats are recommended for Interdur 8802: Interdur 8840, Interdur 8842, Interdur 8860. For other suitable topcoats/intermediate coats, consult International.
| For further information on the industry standards, terms and abbreviations used in this datasheet, see www.international-pc.com | In the following documents on the website: • Definitions and abbreviations • Surface preparation • Coating application • Theoretical and practical spreading rate. These sections are also available as separate publications on request. |
|---|
This product must be applied at the production site by professional applicators in accordance with the recommendations in this manual, the Material Safety Data Sheet and the instructions on the container label. Do not use this product without first reviewing the Material Safety Data Sheet (MSDS) that International Paint provides for its customers.
All work related to the application and use of this product must be carried out in accordance with the relevant national health, safety and environmental standards and regulations.
If welding or flame cutting is required on metal coated with this product, dust and fumes will be generated; use appropriate personal protective equipment and adequate local ventilation.
If in doubt about the suitability of this product, consult International Paint.
| Packaging Specifications | Component A | Component B | ||
| Volume | Packaging | Volume | Packaging | |
| 20 L | 15 L | 20 L | 5 L | |
For other available packaging sizes, contact International Paint.
| Packaging Specifications | Component A | Component B |
| 20 L | 27.6 kg | 5.3 kg |
| Shelf life | At least 12 months at 25 °C (77 °F). Thereafter, inspect before use. |
|---|
Store in a dry, cool environment away from heat and sources of ignition.
The information given in this product data sheet is not exhaustive. Anyone who uses, for any purpose, any product other than those specifically recommended in this data sheet without first obtaining our written confirmation does so at their own risk as regards the suitability of the product for the intended purpose. Although to the best of our knowledge all advice or statements given about the product (whether in this data sheet or otherwise) are correct, we cannot control the quality or condition of the substrate, nor the many factors affecting the use and application of the product. Accordingly, unless we specifically agree otherwise in writing, we accept no liability, to the maximum extent permitted by law, for any product performance problem arising, or for any loss or damage caused by use of the product. We hereby disclaim any warranty or representation, express or implied, arising by operation of law or otherwise, including but not limited to any implied warranty of merchantability or fitness for a particular purpose. All products supplied and all technical guidance provided are subject to our standard terms and conditions of sale. You should obtain a copy of this document and read it carefully. The information contained in this product data sheet may be amended at any time in the light of experience and of our product development policy. Before using the product, it is the customer's responsibility to check with the local representative that the data sheet in their possession is the latest version.
This product data sheet is available on www.international-marine.com or www.international-pc.com and should be identical to this copy. If the version on the website differs from this one, the version on the website shall prevail.
© 2016/8/18 AkzoNobel. All rights reserved.
www.international-pc.com
Data is subject to the manufacturer's latest version; in all cases the manufacturer's latest TDS prevails.
Packaging specifications and batch lead times are subject to actual availability. PleaseContact Uscontact us for project-based calculation.